Modern vertical machining centers (VMCs) often need more than just a powerful spindle and accurate cutting tools to maintain efficient machining. Through-spindle coolant (TSC) and chip conveyors are two important options that can improve machining performance and simplify machine operation, but they serve different purposes.
TSC delivers coolant through the spindle and cutting tool directly to the cutting zone, helping control heat and improve chip evacuation during demanding operations. A chip conveyor, on the other hand, automatically removes chips from the machine work area and transports them to a collection point.
Understanding how these systems work and when they are needed can help manufacturers select a VMC configuration that matches their machining applications, production volume, materials, and long-term maintenance requirements.
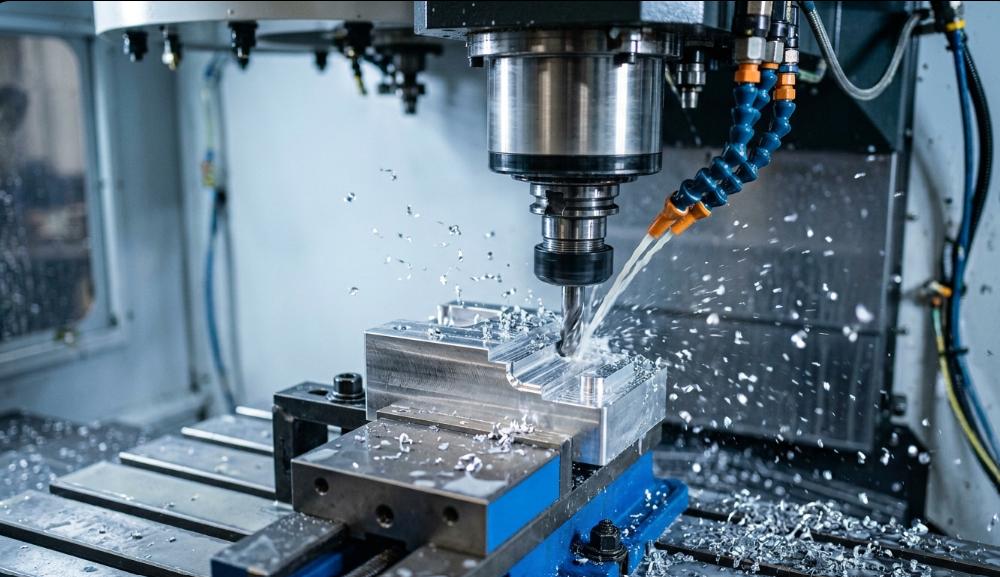
Through-spindle coolant (TSC) is a coolant delivery system designed to send cutting fluid through the machine spindle and, when supported by the tooling, directly through passages in the cutting tool. Instead of relying only on coolant sprayed from external nozzles, TSC brings coolant closer to the actual cutting point.
This is particularly useful when machining deep holes, pockets, or complex features where conventional coolant delivery may not effectively reach the cutting zone. The coolant can help reduce heat generated during cutting while also assisting in pushing chips out of holes and narrow machining areas.
TSC is commonly considered for VMC applications involving demanding drilling, tapping, high-speed machining, or production environments where consistent coolant delivery is important.
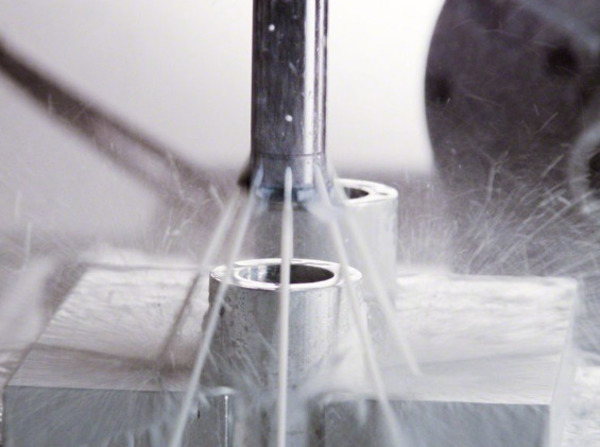
TSC systems can vary depending on coolant pressure, machine configuration, and the machining application. Common considerations include:
The appropriate TSC configuration depends on the cutting tools, workpiece material, machining depth, spindle arrangement, and required coolant flow.
A typical TSC system consists of several components that work together to deliver filtered coolant from the tank to the cutting tool.
The main components generally include:
The exact configuration can vary between VMC models and manufacturers. Therefore, TSC should be selected based on the machine's spindle design and the tooling system in use.
TSC can be valuable when external coolant cannot effectively reach the cutting area. Its main purpose is not simply to supply more coolant, but to deliver it where it can have the greatest effect.
A VMC may benefit from TSC when:
For manufacturers, the decision should be based on actual machining requirements rather than treating TSC as a necessary feature for every VMC.
|
Advantages |
Disadvantages |
|
Delivers coolant closer to the cutting zone |
Higher initial machine cost |
|
Helps with deep-hole chip evacuation |
Requires compatible tooling |
|
Can improve heat management |
Pump and filtration systems require maintenance |
|
Useful for demanding production applications |
Coolant cleanliness becomes more important |
|
Can support consistent machining conditions |
May be unnecessary for simple, low-demand operations |
TSC can provide substantial benefits in the right application, but it also adds equipment, cost, and maintenance requirements. For this reason, manufacturers should evaluate the type of machining they perform before specifying the system.
A chip conveyor is an automated system that collects and removes chips generated during CNC machining. In a VMC, cutting operations can produce a large amount of metal chips, particularly during high-volume production, heavy cutting, and machining of materials such as steel, cast iron, and aluminum. If these chips remain inside the machine, they can interfere with the workpiece, cutting tools, coolant flow, and machine operation.
A chip conveyor transports chips from the machining area to an external collection container or chip bin. This reduces the need for operators to manually clean the machine after frequent machining cycles. For VMC users, a chip conveyor can therefore be an important part of efficient chip management, especially when machining generates a continuous or heavy volume of chips.
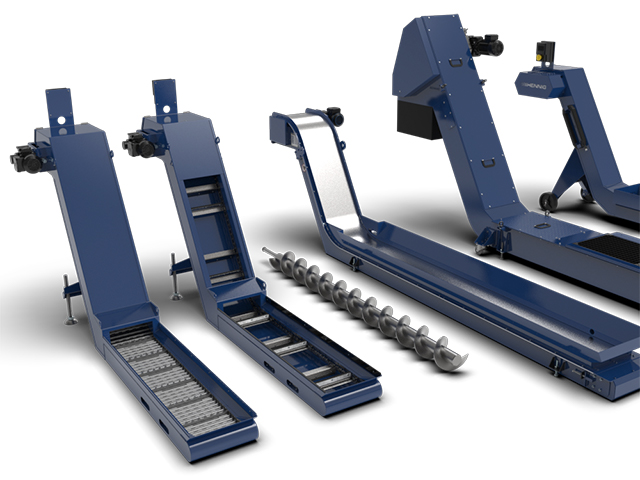
Different chip conveyor designs are available for VMCs, and each type is suited to different chip characteristics and machining applications.
The best conveyor type depends on the workpiece material, chip shape, chip volume, coolant usage, and available machine space.
Although designs vary, a typical chip conveyor consists of several basic components that work together to move chips away from the machining area. The main components generally include:
The conveyor is normally integrated with the VMC so that chips can be removed without requiring the operator to stop machining frequently for manual cleaning.
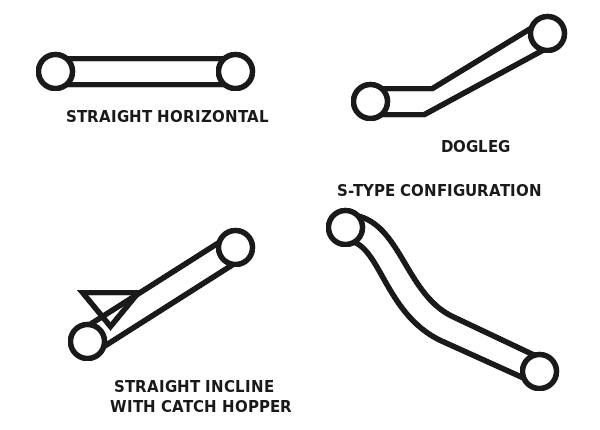
A chip conveyor becomes increasingly useful when a VMC produces more chips than an operator can conveniently remove manually. The decision is particularly relevant for production environments where the machine runs for extended periods.
A VMC may benefit from a chip conveyor when:
For low-volume machining or applications that generate only small amounts of chips, a manual or simpler chip-removal arrangement may be sufficient.
|
Advantages |
Disadvantages |
|
Automatically removes chips from the VMC |
Increases the initial machine cost |
|
Reduces manual cleaning requirements |
Requires additional maintenance |
|
Useful for high-volume machining |
Occupies additional machine or floor space |
|
Helps maintain a cleaner machining area |
Moving components can wear over time |
|
Can support longer unattended production cycles |
The conveyor type must match the chip material and shape |
A chip conveyor can improve productivity and machine cleanliness, but it is not automatically required for every VMC. The right choice depends on chip volume, material, machining method, production schedule, and required level of automation.
Through-spindle coolant and chip conveyors can both improve VMC operation, but they address different machining challenges. TSC focuses mainly on coolant delivery, heat management, and chip evacuation around the cutting tool, while a chip conveyor focuses on removing accumulated chips from the machine.
Understanding these differences makes it easier to determine whether a VMC needs one system, the other, or both.
The two systems have significantly different designs because they perform different functions.
A TSC system is integrated with the coolant and spindle system. It normally includes a coolant pump, filtration system, coolant lines, rotary union, and a spindle passage that allows coolant to reach compatible cutting tools.
A chip conveyor is primarily a mechanical chip-handling system. Depending on its design, it can use a hinged belt, scraper, magnetic mechanism, or screw to transport chips away from the machining area.
Therefore, TSC is closely associated with the spindle, tooling, and coolant system, while a chip conveyor is associated mainly with the machine enclosure, chip collection area, and waste-handling system.
The most important difference is what each system is designed to accomplish.
|
Factor |
Through-Spindle Coolant |
Chip Conveyor |
|
Primary purpose |
Delivers coolant through the spindle/tool |
Removes chips from the machine |
|
Main focus |
Cooling, lubrication, and chip evacuation |
Chip collection and transportation |
|
Works directly with |
Spindle, coolant system, and tooling |
Machine enclosure and chip collection system |
|
Particularly useful for |
Deep holes, demanding cutting, difficult coolant access |
High chip volumes and extended production |
|
Operator benefit |
Helps maintain cutting conditions |
Reduces manual chip removal |
These systems are therefore not direct substitutes for each other. A VMC can use TSC without a chip conveyor, a chip conveyor without TSC, or both, depending on the machining application.
Compatibility is an important consideration before adding either system to a VMC. For TSC, the machine spindle must support the required coolant delivery arrangement, while the tools must have internal coolant passages when coolant is intended to pass through the tool. The coolant pump, filtration system, pressure, and machine control should also match the intended application.
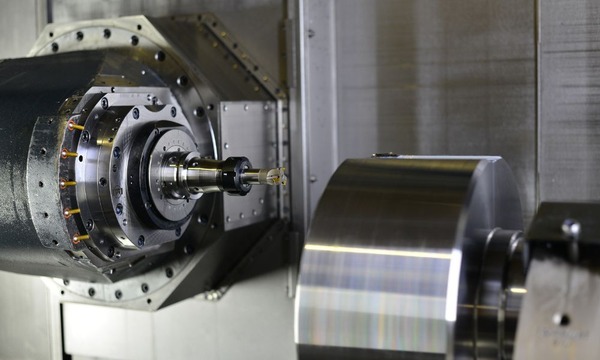
For chip conveyors, compatibility depends on the VMC's physical design, chip outlet arrangement, available space, and the type of chips produced during machining.
Manufacturers should therefore check the machine configuration before selecting either system rather than assuming that every accessory will fit every VMC.
The cost of TSC and chip conveyors varies according to their specifications, capacity, pressure requirements, construction, and integration with the machine. TSC can increase machine cost because it may require a dedicated high-pressure pump, filtration, rotary union, plumbing, and compatible spindle/tooling arrangements.
A chip conveyor also adds cost through its conveyor mechanism, drive motor, control system, and integration with the machine's chip and coolant collection system.
Instead of comparing price alone, manufacturers should consider the machining problem each system solves. An additional feature may provide value when it reduces downtime, manual cleaning, tooling problems, or production interruptions.
TSC installation is closely connected to the VMC's spindle and coolant circuit. Because coolant must travel through the spindle, installation and integration need to be properly matched to the machine's spindle configuration.
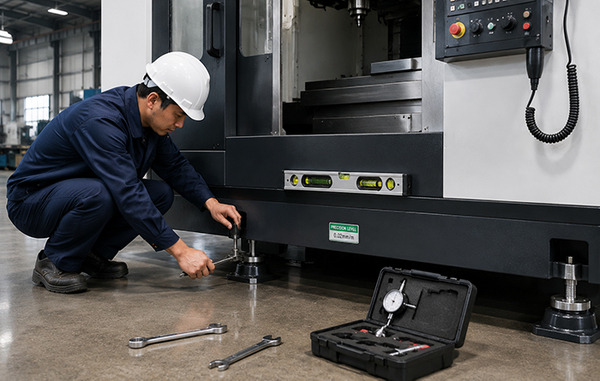
A chip conveyor is generally installed around the machine's chip discharge area and requires suitable physical clearance and electrical/control connections.
Both systems are therefore easier to specify as part of the original VMC configuration. Retrofitting may be possible in some cases, but feasibility depends on the machine design and available space.
Maintenance requirements are also different. TSC requires attention to coolant cleanliness, filters, pumps, seals, and other coolant-delivery components. Contaminated coolant or clogged filtration can affect system performance.
Chip conveyors require inspection of the conveyor mechanism, drive components, bearings or moving parts, and chip accumulation areas. The conveyor should also be checked regularly for excessive wear or blockage.
In both cases, routine maintenance can help prevent avoidable downtime and maintain consistent machine operation.
There is no universal requirement for every VMC. The appropriate configuration depends on what the machine is expected to produce, how frequently it operates, and what type of machining processes it performs.
Start by examining the actual machining operations. If the VMC performs frequent deep-hole drilling, tapping, high-speed cutting, or operations where external coolant cannot effectively reach the cutting zone, TSC may be useful.
If the machine produces a large quantity of chips during milling and runs for long production cycles, a chip conveyor may be more beneficial. For demanding production environments, using both systems can provide advantages: TSC helps manage coolant delivery and cutting conditions, while the conveyor handles accumulated chips.
Workpiece material affects both coolant requirements and chip management. Materials that generate significant heat during cutting may benefit from effective coolant delivery. Materials that produce large quantities of chips may create a stronger need for automated chip removal.
For example, a VMC used for heavy metal removal may require more effective chip handling than a machine performing occasional light machining.
Production volume is another major factor. For low-volume or occasional machining, manually removing chips and using conventional coolant delivery may be adequate.
For continuous or high-volume production, however, automation becomes more valuable. TSC can provide consistent coolant delivery during demanding cycles, while a chip conveyor can reduce the need for frequent manual cleaning.
Before selecting either option, manufacturers should consider ongoing maintenance. TSC requires proper coolant management, filtration, and inspection of its pump and delivery components. Chip conveyors require cleaning and inspection of moving components.
The goal should be to select a system that the maintenance team can properly operate and service throughout the machine's working life.
The budget should be considered together with expected production benefits. A TSC system may be difficult to justify for simple machining where conventional coolant already reaches the cutting area effectively. Similarly, a chip conveyor may not provide significant value if the machine produces very few chips.
For high-production applications, however, reduced manual intervention, improved process consistency, and less downtime may make these accessories worthwhile over the machine's operating life.
The best approach is to compare the additional investment with the VMC's specific productivity and maintenance requirements, rather than selecting an accessory based on price alone.
Q: What is the main difference between through-spindle coolant and a chip conveyor?
A: Through-spindle coolant delivers coolant through the spindle and cutting tool to the machining area, helping with cooling and chip evacuation. A chip conveyor, on the other hand, removes chips from the VMC work area and transfers them to a collection point. They perform different functions and can be used together.
Q: When does a VMC need through-spindle coolant?
A: A VMC may benefit from through-spindle coolant when performing deep-hole drilling, tapping, high-speed machining, or other operations where coolant needs to reach the cutting zone directly. It can also help manage heat and improve chip evacuation from deep or enclosed cutting areas.
Q: When is a chip conveyor useful for a VMC?
A: A chip conveyor is particularly useful when a VMC produces a large amount of chips during continuous or high-volume production. It automatically moves chips out of the machine, reducing the need for frequent manual cleaning and helping maintain a more organized work area.
Q: Can through-spindle coolant and a chip conveyor be used together?
A: Yes. These systems are complementary because they address different machining requirements. Through-spindle coolant delivers coolant to the cutting area, while the chip conveyor removes chips from the machine. Using both can be practical for demanding production applications.
Q: Do all VMC machines require a chip conveyor and through-spindle coolant?
A: No. The requirement depends on the machining application. A VMC used for light-duty machining or small production batches may not need these options, while machines used for deep-hole operations, high chip production, or continuous manufacturing may benefit from them.
Q: What factors should be considered before choosing these VMC options?
A: Consider the type of machining operations, workpiece material, chip volume, production quantity, tooling requirements, machine compatibility, maintenance needs, and available budget. Evaluating these factors helps determine whether through-spindle coolant, a chip conveyor, or both are appropriate for a particular VMC.
Choosing between through-spindle coolant and a chip conveyor depends on matching the machine configuration to your actual machining requirements. Through-spindle coolant can be valuable for operations where effective coolant delivery and chip evacuation are important, while a chip conveyor can help manage chips during continuous or high-volume machining. In some applications, using both can provide a more complete machining setup.
If you already have your part drawings, material information, tooling requirements, and production details, you can use them to select the right VMC configuration.
Contact CNC Yangsen to discuss your machining requirements and find a suitable CNC machining solution for your production needs.
Tags :